Featured OEM/ODM Product Offerings
Explore our high-demand contact lens product catalog and companion medical-grade eye care accessories engineered for global distribution and custom private labeling.
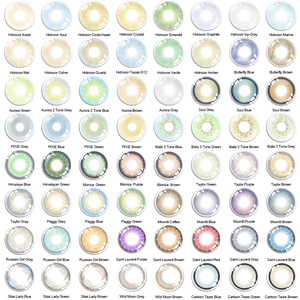
1. Strategic Enterprise Infrastructure & CE Regulatory Framework
In the rapidly expanding global ophthalmic and ocular cosmetics industry, the integrity of companion contact lens cases and custom eye cases serves as a primary pillar of patient safety, brand reputation, and regulatory compliance. Stephies Lens CO.,LTD stands at the forefront of this sector as a premier B2B manufacturer and specialized supplier, providing fully compliant CE Certified Custom Eye Cases alongside world-class OEM/ODM contact lens production capabilities.
Navigating international medical device directives—specifically the European Union’s Medical Device Regulation (EU) 2017/745 (MDR) and ISO 13485:2016 quality management frameworks—requires absolute manufacturing discipline. Standard injection molding facilities often fail to prevent micro-leakage, chemical leaching, and microbial contamination. By contrast, our dedicated production matrix operates within Class 100,000 dust-free cleanrooms, utilizing high-precision multi-cavity tooling and bio-compatible, medical-grade virgin polymers (US FDA & USP Class VI compliant).
Stringent CE Mark Compliance
Full technical documentation, biocompatibility testing (ISO 10993 cytotoxicity, sensitization), and ongoing EU MDR compliance validation for frictionless global import.
Automated Precision Tooling
Computer-controlled micro-injection molding with ultra-tight tolerance thresholds (±0.01mm) ensuring zero thread slippage, fluid leakage, or structural warping.
End-to-End Turnkey OEM/ODM
From initial industrial design renders and 3D prototyping to custom resin color matching, hot-stamping, UV printing, and retail-ready sterile blister packaging.
2. B2B Technical Specifications & Material Engineering Matrix
When global distributors and cosmetic brand managers evaluate custom eye cases, material science plays a decisive role. Contact lens solutions contain active disinfectants and delicate saline buffering agents that must remain stable without absorbing toxic plasticizers or phthalates. Below is an engineering overview of our proprietary material configurations:
| Case Category | Material Composition | Sealing Architecture | Thermal & Sterilization Resistance | Compliance Credentials |
|---|---|---|---|---|
| Standard Screw-Cap Cases | Medical Polypropylene (PP) Body + PE Cap | Precision Double-Thread Seal | Up to 121°C Autoclave / EO Gas | CE Mark, FDA Listed, ISO 10993 |
| Ergonomic Travel Companion Kits | Impact ABS Shell + PP Inner Vials | Interlocking Gasket + Soft TPE Insert | Ethylene Oxide (EO) Sterilized | CE MDR (Class I), REACH, RoHS |
| Custom Mirror & Care Sets | Eco-Friendly Recyclable PP + Glass Mirror | Magnetic / Snap-Latch Lock | Standard Chemical Disinfection | CE Certified, BPA-Free, Phthalate-Free |
| Ultrasonic Hydro-Sonic Clean Cases | ABS Housing + Medical Grade Silicone Reservoir | Hermetic O-Ring Barrier | IPX7 Water Resistance Structural Rating | CE, FCC, RoHS Medical EMC Compliance |
Every standard and custom eye case manufactured by Stephies Lens undergoes rigid 100% pneumatic pressure leak-testing (under 50kPa water submersion) to guarantee that no solution loss or oxidation occurs during transit, air travel, or daily consumer carry.
3. Strategic Sourcing & Procurement Trends (2026–2030)
As the eye care market transitions toward elevated consumer safety standards and eco-conscious consumption, B2B buyers must align their procurement strategies with several overarching global shifts:
1. Transition to Bio-Based & Circular Polymers
Global regulatory bodies are increasingly favoring suppliers using ocean-bound recycled plastic matrices, biodegradable PLA compounds, and mono-material recyclable PP structures to meet net-zero corporate obligations.
2. Nano-Antimicrobial Surface Integration
Leading brand owners are shifting away from passive plastic cases toward active antimicrobial surfaces embedded with silver-ion nano-fillers that inhibit bacterial biofilm growth (such as Pseudomonas aeruginosa) on inner case walls.
3. Automated Integrated Bundling
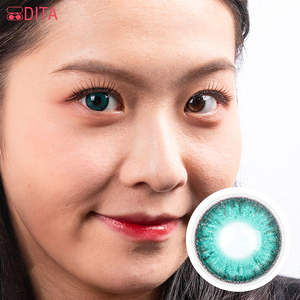
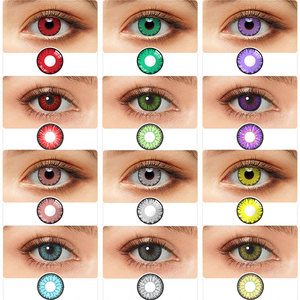
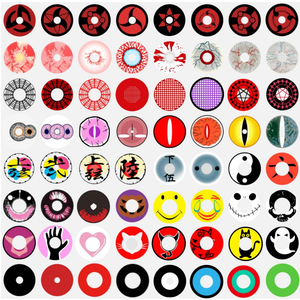
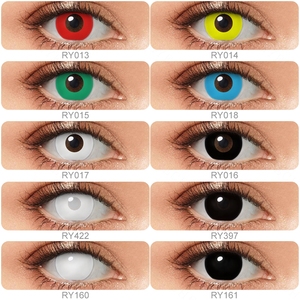
Distributors are moving away from single-item sourcing. Purchasing managers prefer automated one-stop manufacturing partners who bundle custom cases, soft contact lenses (Natural, Prescription RX, or FX Cosplay), rewetting drops, and application tools under one CE certificate.
4. Product Evolution & Smart Manufacturing Innovations
The humble contact lens case has evolved from a simple plastic reservoir into an engineered medical delivery accessory. Historical design flaws—such as sharp internal corner ridges that tear delicate silicone hydrogel lenses or loose threads that cause solution leakage—have been eliminated through computer-guided fluidic engineering.
At Stephies Lens, our automated production lines integrate In-Mold Labeling (IML) and high-speed robotic pick-and-place assembly. This ensures that customized artwork, brand logos, and batch tracking QR codes are permanently embedded into the polymer matrix rather than printed with surface inks that erode when exposed to multipurpose lens solutions. Furthermore, our modern custom eye case series features rounded convex lens wells, allowing consumers to easily retrieve lenses without fingernail damage or edge inversion.
5. Frequently Asked Sourcing & Technical Procurement FAQs
Answers to essential technical, compliance, and logistics questions from professional procurement officers and brand founders evaluating custom eye case suppliers:
Why is CE Certification mandatory for custom eye cases sold in international markets?
Under the European Medical Device Regulation (EU MDR 2017/745), contact lens storage cases are classified as Class I / Class Is medical device accessories. CE certification verifies that the case material is bio-compatible, free of chemical leaching hazards, and capable of maintaining sterile integrity without damaging soft or rigid gas-permeable (RGP) lenses. Importing non-CE certified eye cases into regulated territories risks customs seizure and product liability claims.
What is the typical minimum order quantity (MOQ) for custom-molded eye cases versus private-label logo printing?
For existing catalog shapes requiring custom logo printing (silk screening, hot-stamping, or UV digital printing), our factory supports agile emerging brands with accessible low MOQs starting from 500 to 1,000 units. For fully bespoke custom-molded cases requiring dedicated injection mold tooling, typical MOQs start at 10,000 units to amortize engineering and steel tooling costs efficiently.
Can your factory produce custom eye cases suitable for silicone hydrogel and high-water content lenses?
Yes. All our medical PP and liquid silicone storage wells undergo rigorous extractable and leachable (E&L) safety testing. Our formulations are 100% compatible with multipurpose disinfectants, peroxide systems, and high-water content (38% to 58%) hydrogel or silicone hydrogel colored contact lenses without causing parameter swelling or lens dehydration.
What lead times can buyers expect for custom private label orders and sample evaluation?
Stock catalog samples and color chips are dispatched within 24 to 48 hours for rapid laboratory evaluation. Custom private-label logo printing runs are completed within 7 to 12 business days. For turnkey ODM projects requiring new mold tooling, prototype sampling takes 15 to 20 days, followed by mass production within 20 days post-approval.
How does Stephies Lens guarantee leak-proof sealing during air transport cargo pressurization?
Our cases feature engineered multi-pitch continuous screw threads paired with precision TPE or silicone internal sealing rings. Batch samples are tested inside vacuum chambers under -0.08MPa negative pressure conditions to simulate high-altitude air freight cargo holds, guaranteeing absolute zero leakage.
What customized accessory options can be included within complete custom eye care kits?
We supply fully integrated companion kits including custom outer carrying cases with mirrors, specialized soft-tipped suction sticks, hygienic lens tweezers/forceps, mini solution rewetting drop bottles (10ml), and outer retail color boxes with custom barcodes and tamper-evident seals.
What quality documentation is provided with bulk factory shipments?
Every commercial order is accompanied by a comprehensive Quality Assurance Dossier including a Certificate of Analysis (CoA), Material Safety Data Sheet (MSDS), Bio-compatibility Test Reports (ISO 10993), CE Declaration of Conformity (DoC), and Batch Sterilization Certificates upon request.
Accelerate Your Brand Growth with a Certified Industry Leader
Partner with Stephies Lens CO.,LTD to streamline your supply chain, access competitive factory-direct pricing, and launch custom CE-certified eye cases and contact lens lines with absolute confidence.